Why we deburr every part by hand
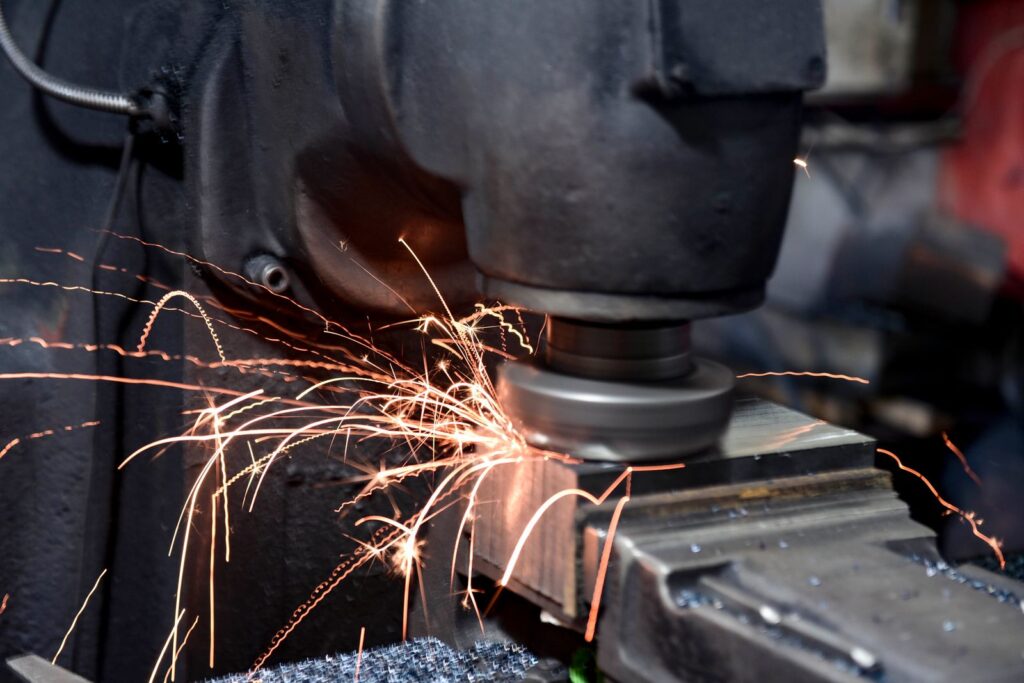
Machining leaves small burrs where a tool exits the metal. On a hydraulic block a burr in a gallery can break loose and score a valve (sample note).
That is why nearly every route card in our shop has a bench operation after machining: ports are checked with a light and a mirror, edges are broken, and the part is washed before inspection.
If your drawing asks for a specific edge break, such as 0.2 to 0.5 mm, we measure it at inspection like any other dimension.